Project Overview
A renowned Brazilian diversified food group, whose sauces and tinned products are exported to markets across South America and Europe, decided to carry out a comprehensive upgrade of its factory’s steam supply system to meet growing production capacity demands, reduce energy consumption per unit of output, and actively support the local government’s industrial emissions reduction and energy efficiency improvement initiatives.
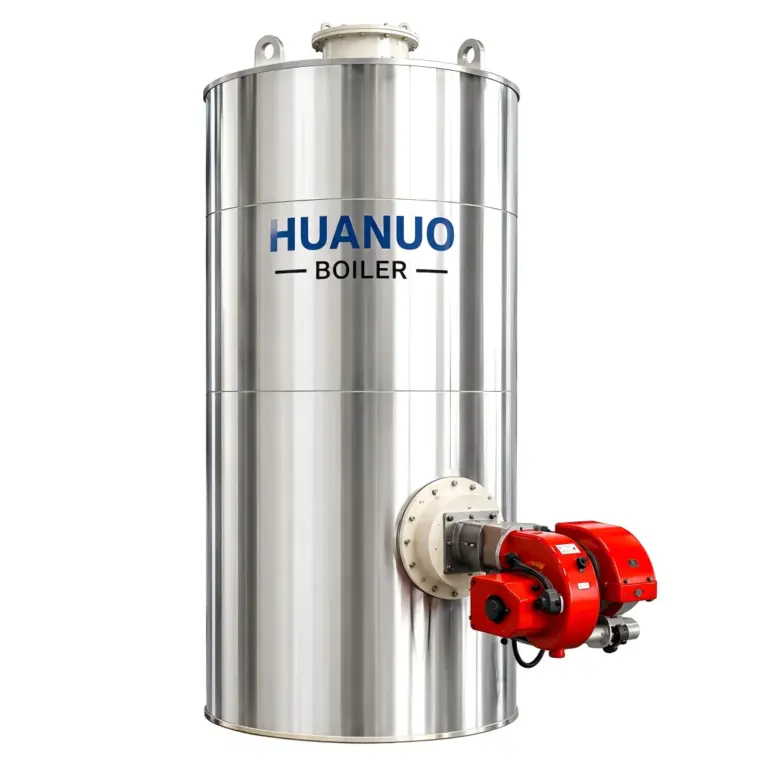
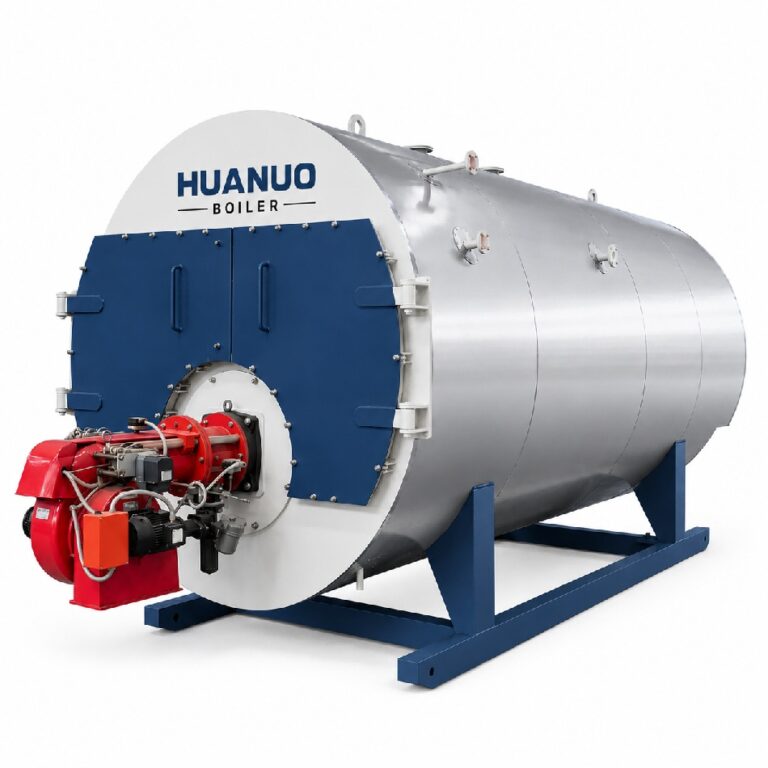
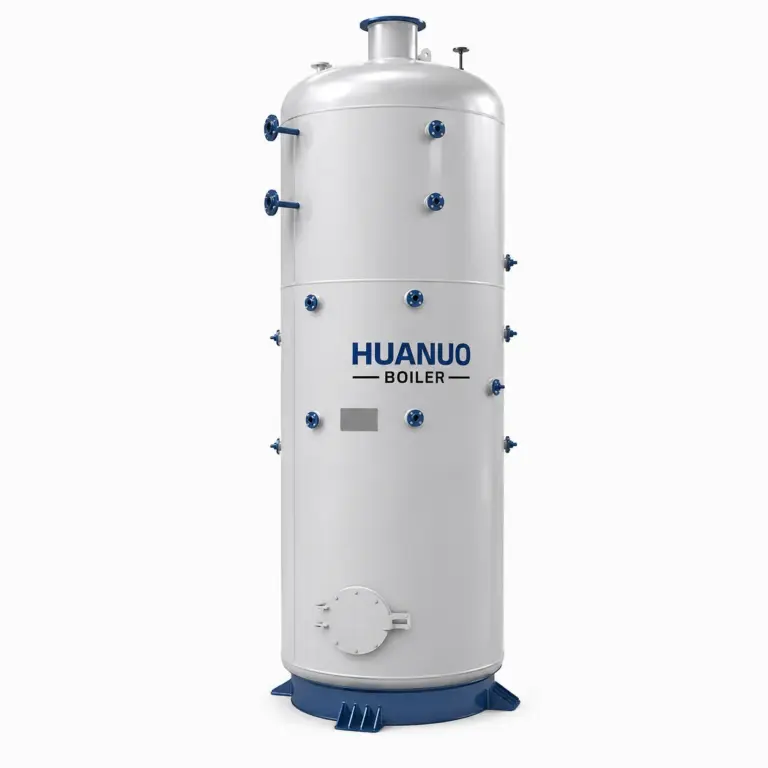
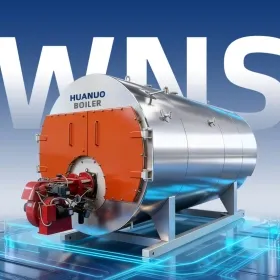
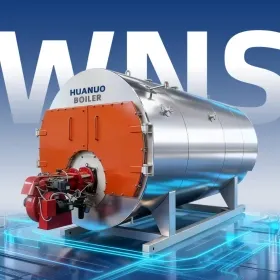
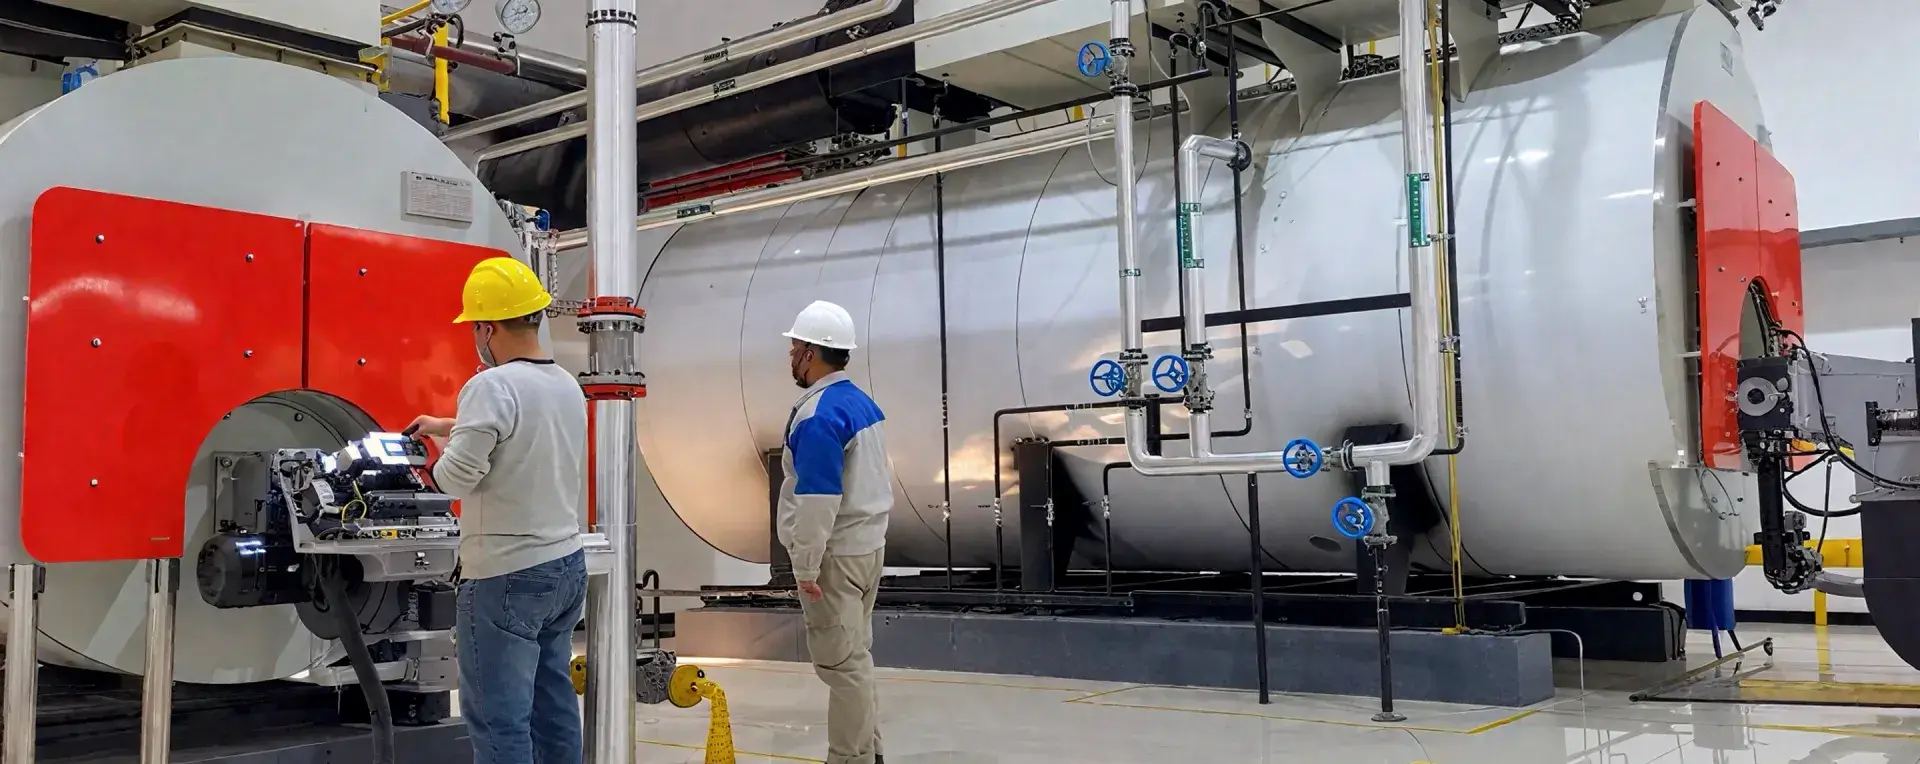
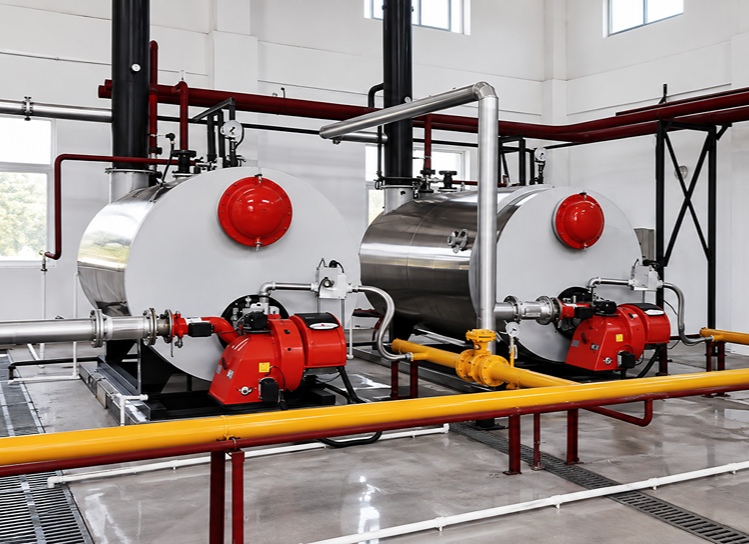
Following rigorous technical evaluations and a global supplier comparison, the group ultimately selected the WNS series low-nitrogen integrated condensing steam boiler solution provided by Huanuo Boilers to establish an intelligent steam supply system comprising both main and auxiliary units. The project comprises one WNS12-1.25-Q and one WNS2-1.25-Q unit, with a total evaporation capacity of 14 tonnes per hour, fully replacing the existing ageing boiler equipment.
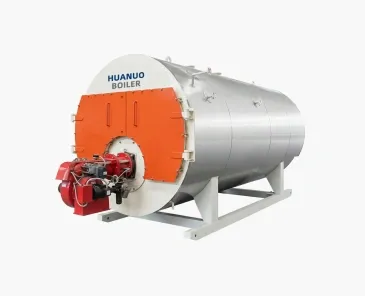
WNS12-1.25-Q
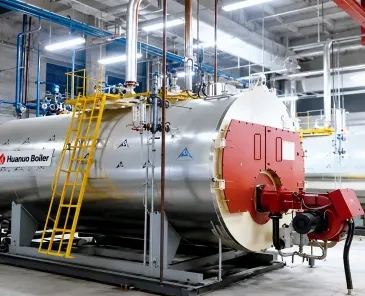
WNS12-1.25-Q
Solution
In response to the factory’s significant fluctuations in peak and off-peak steam demand, as well as its high requirements for steam dryness and stability, Huano Boilers’ technical team proposed an integrated operating strategy of ‘the larger boiler ensuring primary supply, whilst the smaller boiler adjusts the load’:
Request a Solution
The boilers feature a bottom-mounted furnace, a corrugated furnace tube and an integrated two-pass flue gas condensing structure. With a large heat transfer area and compact design, their flue gas exhaust temperature is significantly lower than that of conventional boilers, achieving a thermal efficiency of up to 99 per cent and meeting international Class 1 energy efficiency standards.
Equipped with an advanced load-adaptive control system, it automatically adjusts the start/stop status and combustion ratios of the large and small boilers according to real-time steam demand on the production line, enabling efficient operation across a wide load range of 10%–100% and completely eliminating energy wastage at low loads.
Utilising fully automated low-NOx combustion technology, NOx emissions are well below local environmental regulatory limits, assisting customers in successfully passing environmental audits and fulfilling their commitment to green manufacturing.
The boiler achieves rapid temperature and pressure build-up, whilst the graphical user interface supports multiple languages; local operations and maintenance personnel can independently carry out daily management and maintenance after a short training period.
Core Project Advantages
Overall energy consumption of the steam system is reduced by over 18 per cent, significantly cutting production energy costs.
Intelligent coordination between the main and auxiliary boilers substantially improves pressure stability during the canning sterilisation process—where steam demand fluctuates dramatically—eliminating batch defects caused by fluctuations in steam quality.
Fully automated operation and multiple safety interlock protections enable unattended, safe operation of the equipment.
The tail-end condensate recovery system further utilises waste heat from flue gases, reducing carbon emissions by hundreds of tonnes annually and helping the client meet its ESG targets.
Client Testimonial

Carlos M.
Director of Plant Operations

Carlos M.
Director of Plant Operations
Carlos M.
Director of Plant Operations
Carlos M.
Director of Plant Operations