Project Overview
An international general hospital in Bangkok is a major comprehensive medical institution in the area, with an average daily outpatient volume exceeding 3,000 visits and over 800 inpatient beds. It places extremely high demands on the stability and environmental sustainability of its heating and hot water supply systems. Previously, the hospital’s traditional gas-fired boilers exceeded nitrogen oxide emission limits, making it difficult to comply with increasingly stringent local environmental regulations. Additionally, the equipment generated significant noise during operation, disturbing patients’ rest, and suffered from issues such as large fluctuations in water temperature and high energy consumption. To address these challenges, the hospital conducted extensive research and evaluations before ultimately selecting two low-nitrogen vacuum hot water boilers supplied by Huano Boilers to comprehensively upgrade its heating system.
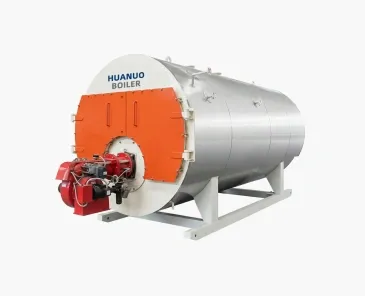
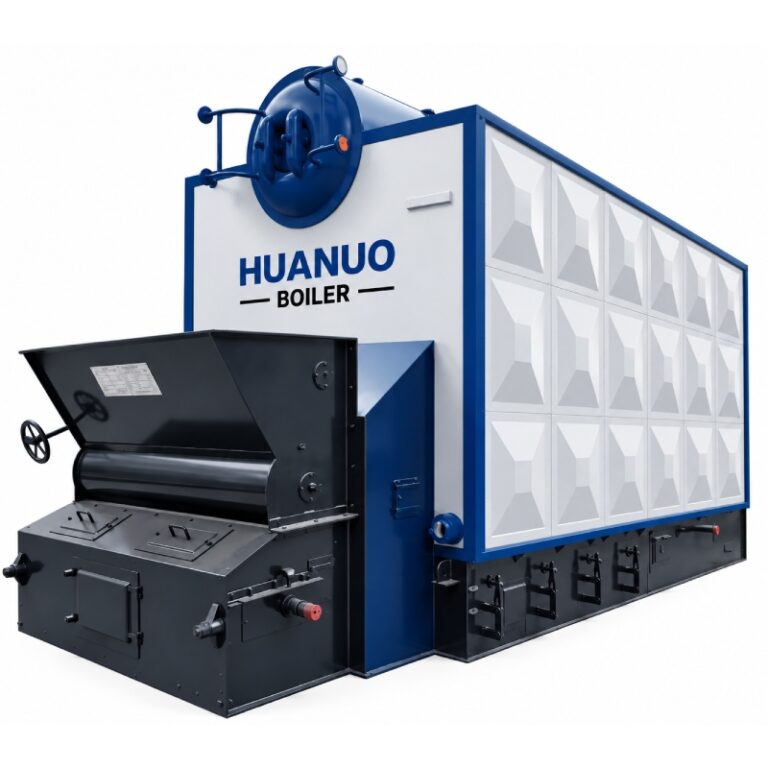
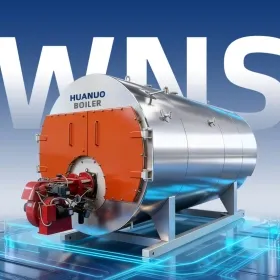
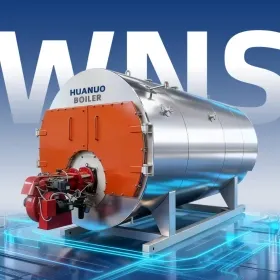
WNS12-1.25-Q
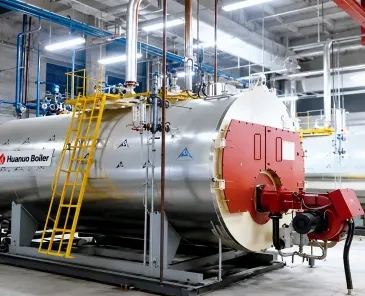
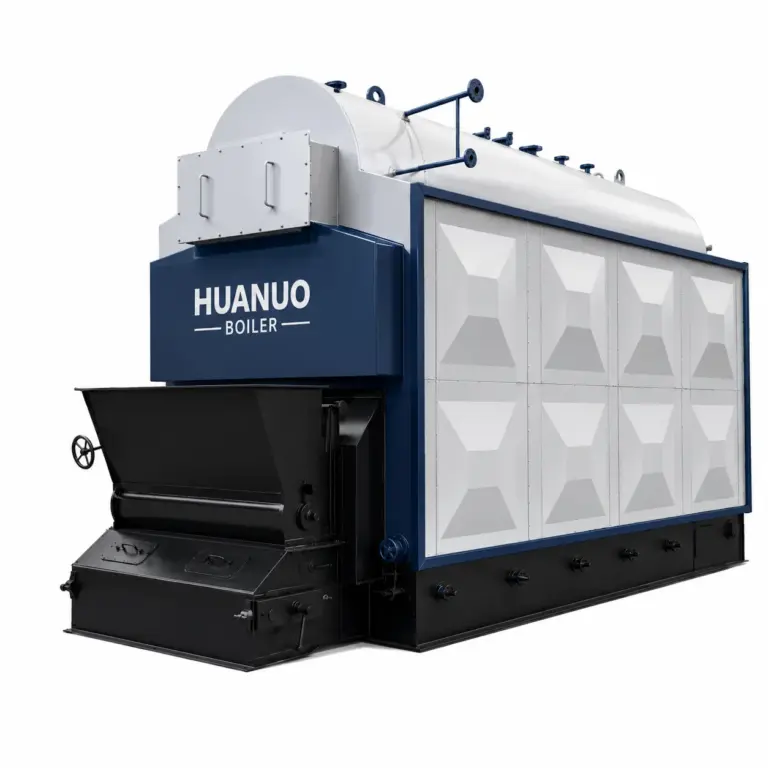
WNS12-1.25-Q
Solution
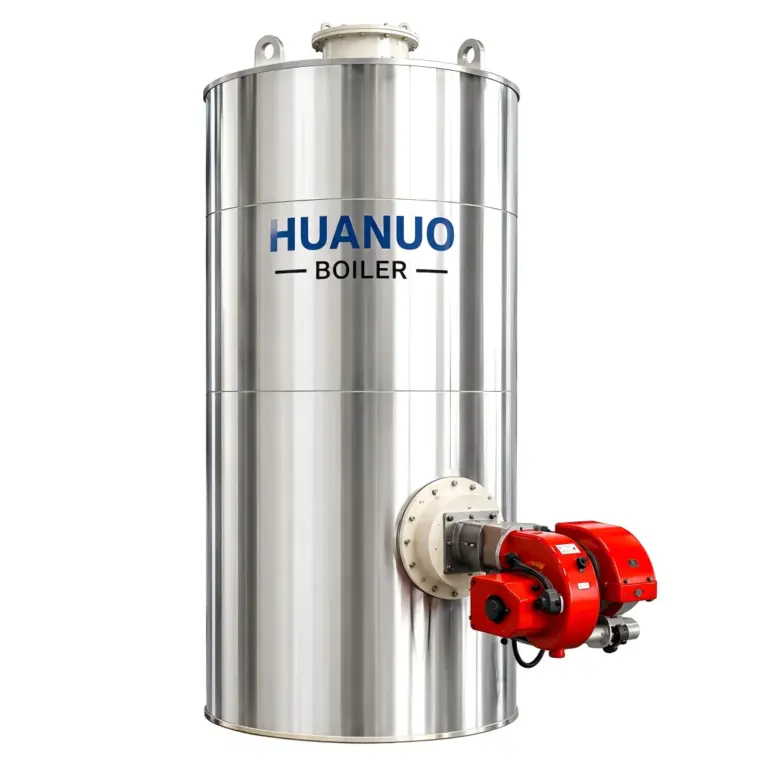
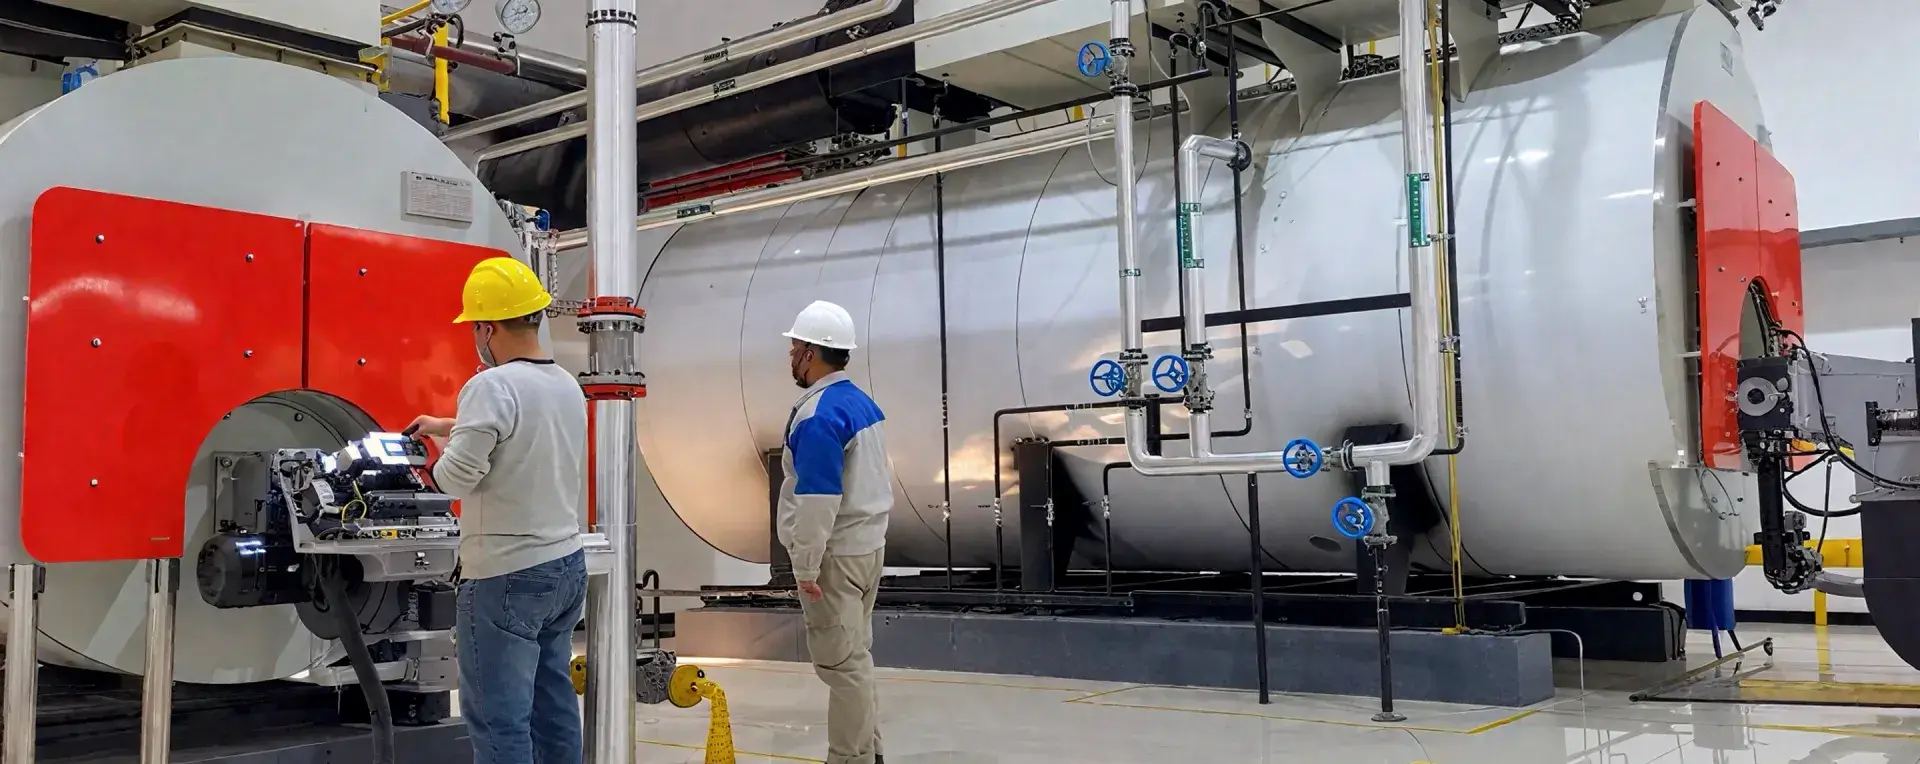
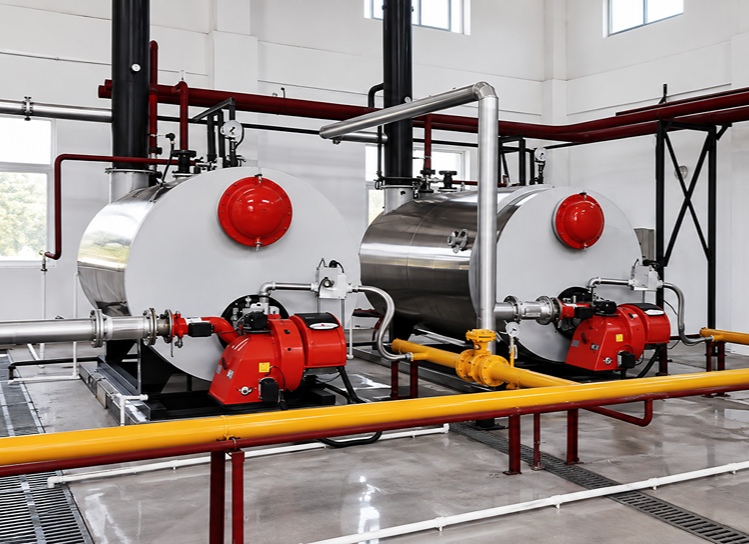
To meet the hospital’s needs for round-the-clock constant-temperature heating, domestic hot water, and specialized heating requirements in medical areas, Huano Boilers configured two ZKS1.75-85/60-Q low-nitrogen vacuum hot water boilers for this project:
Request a Solution
The boilers utilize fully pre-mixed combustion technology, reducing nitrogen oxide emissions to below 30 mg/m³—far exceeding local environmental standards—and passing environmental agency inspections on the first attempt.
The vacuum operation design maintains a constant negative pressure inside the furnace, eliminating the risk of explosion and ensuring the safety of hospital staff and equipment from the source.
Equipped with a dedicated quiet combustion device, operating noise is kept below 55 decibels, making it fully suitable for areas requiring a quiet environment, such as patient rooms and operating rooms.
The intelligent temperature control module precisely maintains water temperature within a range of ±1°C, ensuring stable heating in areas such as patient rooms and operating rooms and preventing water temperature fluctuations.
The boiler’s optimized design features ample heat transfer surface area and high thermal efficiency. Combined with intelligent load regulation, this significantly reduces gas consumption.
Core Project Advantages
Successfully passed inspections by local environmental protection authorities, completely resolving the issue of excessive emissions.
Annual gas cost savings exceed $20,000, resulting in a significant reduction in operating costs.
Stable hot water supply and low noise levels have effectively improved the patient experience, earning unanimous praise from medical staff.
The equipment is easy to operate and runs safely and reliably, providing a solid foundation for the hospital’s efficient operations.
Client Testimonial

Somsak K.
Head of Facilities Management

Carlos M.
Director of Plant Operations
Carlos M.
Director of Plant Operations
Carlos M.
Director of Plant Operations